By Admin / 3 Aug 2026
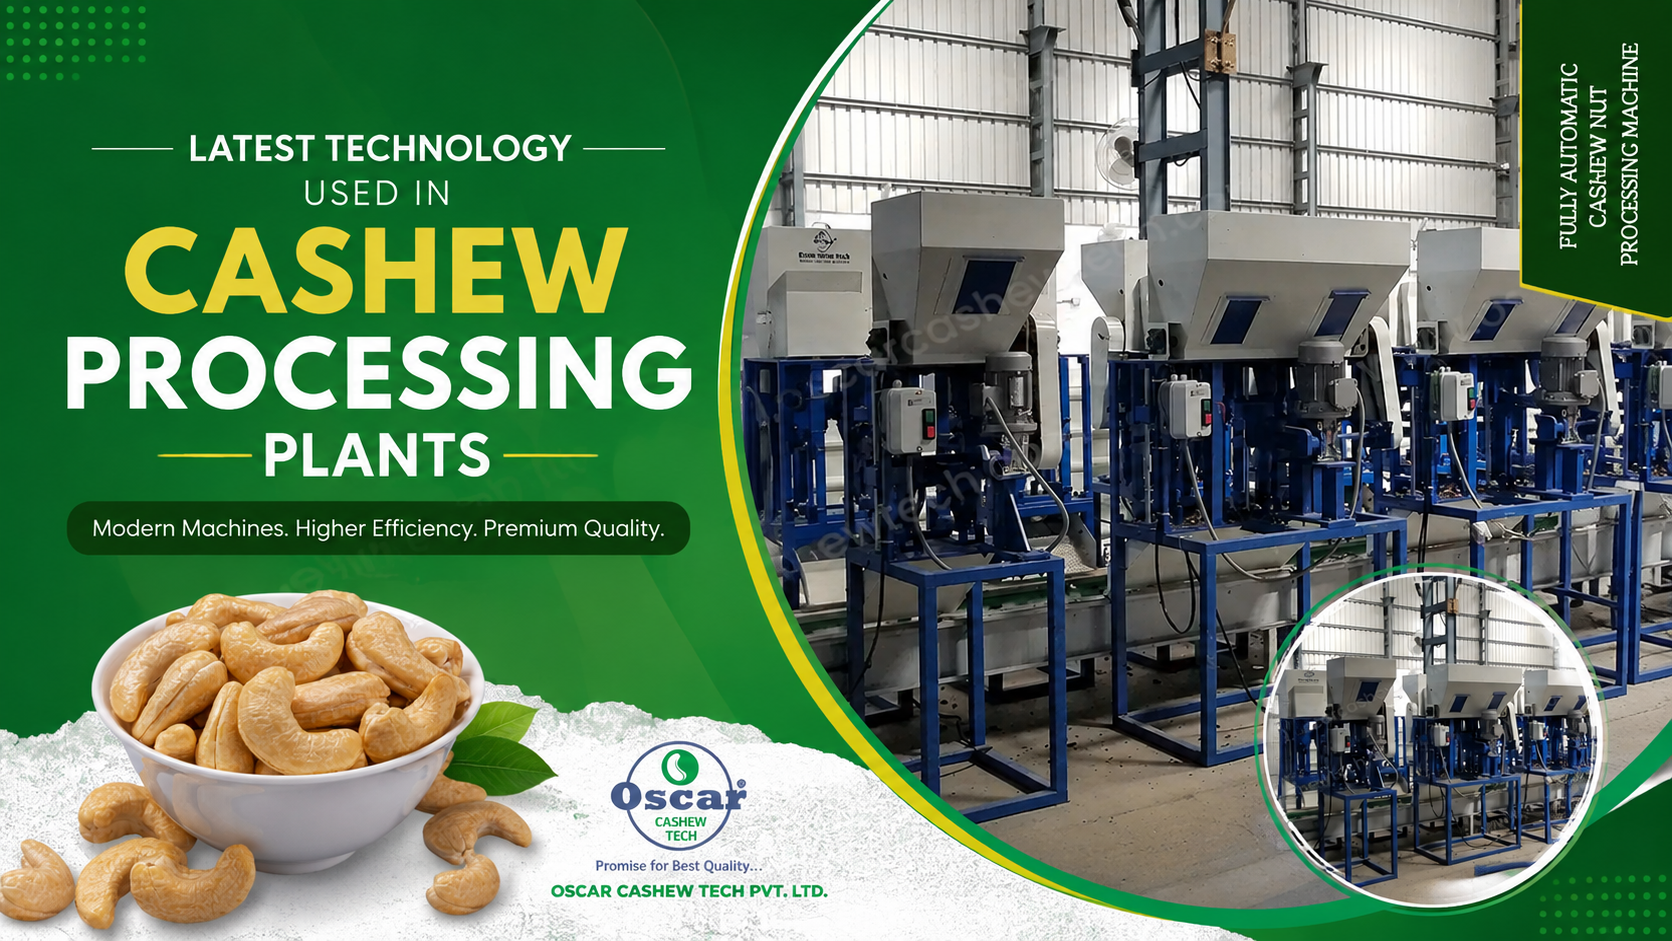
The cashew processing industry has evolved significantly over the years, shifting from traditional manual methods to highly advanced, automated systems. With increasing global demand for high-quality cashew kernels, manufacturers are adopting modern technologies to improve efficiency, reduce labor costs, ensure hygiene, and maximize yield. Today, a modern cashew processing plant integrates precision machinery, automation, and quality control systems to deliver consistent and export-grade products.
One of the most important technological advancements in cashew processing is the development of automated shelling machines. Traditionally, shelling was done manually, which was labor-intensive and time-consuming. Modern shelling machines are designed to break the cashew shells with minimal damage to the kernels.
These machines use adjustable blades and sensors to handle different nut sizes, ensuring higher efficiency and reduced wastage. The automation not only improves productivity but also enhances worker safety by minimizing direct contact with cashew shell oil, which can be harmful.
Steam cooking technology has replaced traditional roasting methods in many advanced plants. In this process, raw cashew nuts are steamed in high-pressure chambers, which helps in loosening the shell and makes it easier to remove.
Modern steam boilers and roasting systems are equipped with temperature and pressure control features, ensuring uniform cooking. This results in better kernel quality, improved color, and reduced breakage during shelling. Additionally, these systems are energy-efficient and environmentally friendly.
Peeling is a delicate process where the thin skin (testa) is removed from the cashew kernel. Earlier, this was done manually, but now automatic peeling machines are widely used.
These machines use compressed air technology to gently remove the skin without damaging the kernel. The result is faster processing, improved hygiene, and consistent output quality. Automated peeling also reduces dependency on skilled labor and speeds up the entire production process.
Drying is a critical step in cashew processing as it reduces moisture content and improves shelf life. Modern drying systems use hot air circulation technology with precise temperature control.
These dryers ensure uniform drying across all kernels, preventing issues like over-drying or uneven moisture levels. Some advanced systems also include energy recovery features, making them cost-effective and sustainable for long-term operations.
Quality grading plays a crucial role in determining the market value of cashew kernels. Advanced color sorting machines use optical sensors and AI-based technology to classify kernels based on color, size, and quality.
These machines can detect defects, discoloration, and broken pieces with high accuracy. By automating the grading process, manufacturers can ensure consistency, reduce human error, and meet international quality standards required for export markets.
Packaging technology has also seen major improvements in modern cashew processing plants. Vacuum packaging machines are widely used to preserve freshness and extend shelf life.
These machines remove air from the packaging, preventing oxidation and moisture absorption. Some systems also use nitrogen flushing to maintain product quality during storage and transportation. This is especially important for export-oriented businesses where long shipping durations are involved.
Modern plants use automated conveyor systems to move raw materials and processed products between different stages. These systems reduce manual handling, improve workflow efficiency, and maintain hygiene standards.
Conveyor belts made from food-grade materials ensure contamination-free processing. Integration with different machines also allows smooth and continuous operations, reducing downtime and increasing overall productivity.
Programmable Logic Controllers (PLC) and SCADA (Supervisory Control and Data Acquisition) systems are transforming cashew processing into a smart and automated operation.
These technologies allow operators to monitor and control the entire plant from a centralized system. Parameters such as temperature, pressure, processing time, and machine performance can be tracked in real time. This ensures better process control, reduces errors, and improves efficiency.
Modern cashew processing plants also focus on sustainability by utilizing waste products efficiently. Cashew shells are used to extract Cashew Nut Shell Liquid (CNSL), which has industrial applications in paints, coatings, and lubricants.
Advanced extraction technologies ensure maximum recovery of CNSL while minimizing environmental impact. This not only adds an additional revenue stream but also promotes eco-friendly operations.
With strict global food safety regulations, modern plants are designed to meet international hygiene standards. Stainless steel equipment, automated cleaning systems, and controlled environments help maintain product safety.
Many processing units also implement HACCP (Hazard Analysis and Critical Control Points) and ISO certifications to ensure quality compliance. These systems enhance consumer trust and open doors to global markets.
 Number 299/2, Dharti Industrial Park, Indore - Ahmedabad Hwy, Near Mahakali Hotel, Ahmedabad, Gujarat 387610
 +91 9924277155+91 9925500380+91 9714477155
 [email protected][email protected][email protected]

Request A Quote